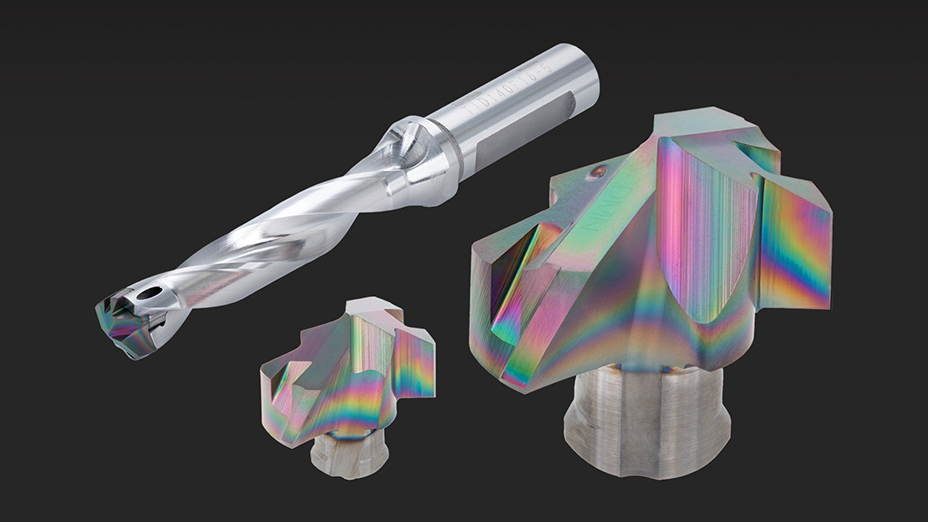
Iwaki, Japan – October, 2026 – Tungaloy Corporation (President: Satoshi Kinoshita, Head Office: Iwaki City, Fukushima Prefecture) has expanded its DrillMeister exchangeable-head drill tool system by adding the DS2025 DLC-coated grade to the DMN drill head line, strengthening its lineup for non-ferrous metal machining. This addition contributes to high-speed, high-efficiency machining of lightweight components and semiconductor parts.
Challenges and Trends
Demand for non-ferrous metal parts and components is increasing, particularly for use in semiconductor manufacturing equipment, electrical and electronic components, and automotive parts. The machining of these materials presents challenges such as built-up edge formation and difficulties in chip evacuation. There is also growing demand for exchangeable-head drilling tools that reduce reliance on costly solid carbide drills while addressing these machining challenges.
Product Overview
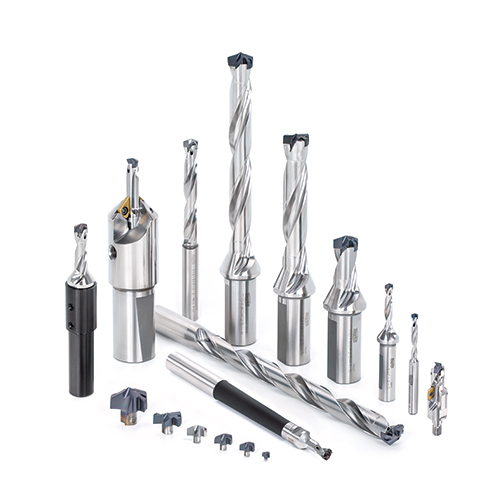
The DrillMeister exchangeable-head drilling tool system, featuring exchangeable drill heads, not only enables highly repeatable drilling by using cutting tips with the same geometry each time, but also offers a wide range of options to accommodate various hole diameters and machining depths.
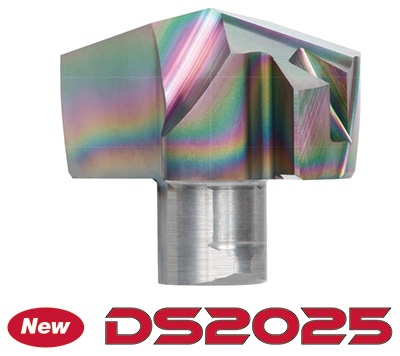
A new DLC (diamond-like carbon)-coated grade, DS2025, has been added for non-ferrous metal machining, enabling higher productivity and longer tool life.
Benefits and Features
Feature 1: Excellent resistance to built-up edge and long tool life
– DS2025, a DLC-coated grade, provides an excellent balance of chipping resistance and wear resistance.
– Significantly reduces built-up edge formation during non-ferrous metal machining, maintaining a consistently sharp cutting edge over an extended period.
– Contributes to long tool life and process stability, especially when machining materials such as aluminum and copper alloys, which are prone to built-up edge.
Feature 2: Improved drilling reliability through excellent chip control
– Reduces friction at the cutting edge during drilling, helping maintain a stable chip shape and contributing to improved chip evacuation.
– The drill tip incorporates a sharp-edge geometry that provides good edge integrity, reducing cutting load and heat generation.
– These features reduce the risk of chip clogging and tool breakage, enabling reliable drilling operations.
Feature 3: Existing TID bodies can be used
– The new drill heads fit existing TID bodies without any modification.
– Simply replacing the drill head enables a smooth transition to non-ferrous metal machining.
Cutting Performance
■ Short and manageable chips in non-ferrous metals
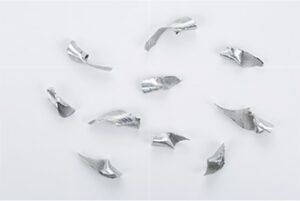
Aluminum alloy (A5052)
| Tool | ø14 mm, L/D = 5 |
| Drill head | DMN140 |
| Grade | DS2025 |
| Cutting speed | Vc = 300 m/min |
| Feed | f = 0.25 mm/rev |
| Hole depth | H = 30 mm |
| Coolant | Wet |
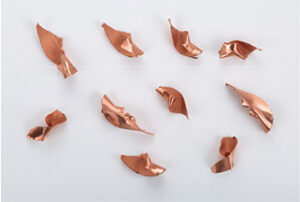
Copper (C1020)
| Tool | ø14 mm, L/D = 5 |
| Drill head | DMN140 |
| Grade | DS2025 |
| Cutting speed | Vc = 200 m/min |
| Feed | f = 0.15 mm/rev |
| Hole depth | H = 30 mm |
| Coolant | Wet |
■ DLC coating blocks material adhesion, maintaining edge sharpness
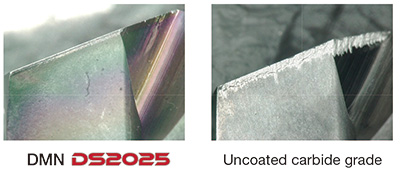
| Tool | ø10 mm, L/D = 3 |
| Drill head | DMN100 DS2025 |
| Grade | Aluminum die casting alloy ADC12 |
| Cutting speed | Vc = 200 m/min |
| Feed | f = 0.3 mm/rev (Through) |
| Hole depth | H = 30 mm |
| Coolant | Wet |
| Machining time | 15 min |
Success Stories
IMPROVED TOOL LIFE
Productivity is tripled by using a dedicated head that can be applied with the same tool body.
| Industry | Engineering | |
| Component | Electric parts | |
| Material ISO code |  Non-ferrous metal |
|
| Work material | A5052 | |
| Machine(Spindletype) | Vertical Machining Center | |
| Tool family | Holemaking | |
| Toolcategory | Drilling | |
| Product name | DrillMeister | |
| TSR No. | 5686H |