



Cermet grades for steel finishing turning
Cermet grades with remarkable stable tool life due to incredible fracture resistance
Applications & Features
Applications
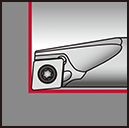
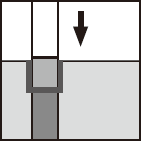
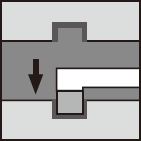
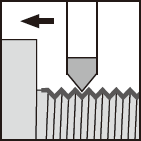
Features
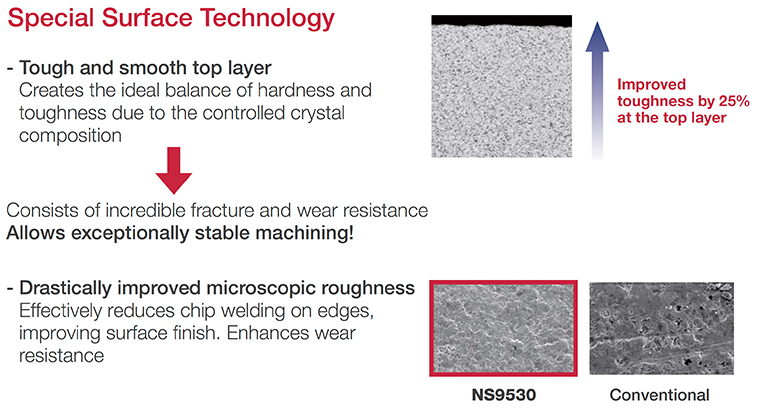
1. Special Surface Technology
Consists of incredible fracture and wear resistance for exceptionally stable machining!
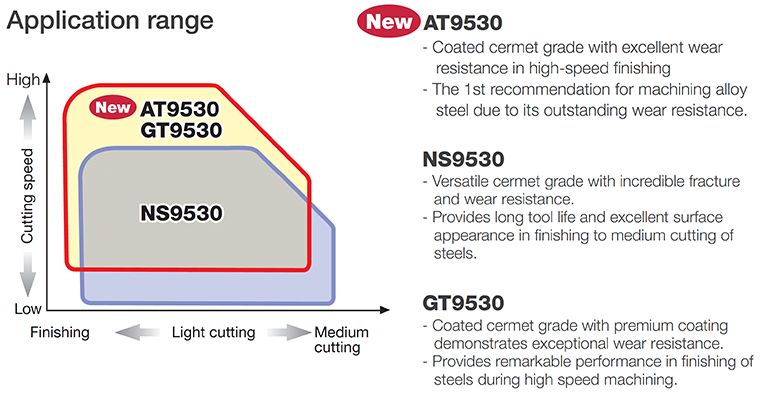
2. Application range
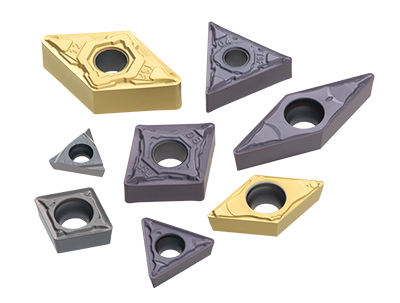
Grades
NS9530


- High fracture resistance
- Suitable for finishing to medium cutting of steel
GT9530
- High wear resistance
- Excellent surface quality in finishing
AT9530
- High wear resistance
- First choice for machining alloy steel
Practical examples
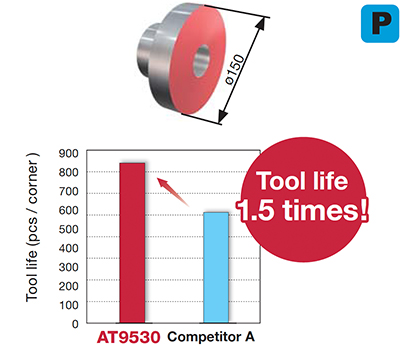
Example #1
General Engineering
| Part: | Rotor parts |
| Material: | Sintered material |
| Insert: | VNMG160402-TSF |
| Grade: | AT9530 |
| Cutting conditions: | Vc = 220 (m/min) f = 0.07 (mm/rev) ap = 0.5 (mm) Application: Face turning (Continuous cutting) Coolant: Wet |
Example #2
Automotive Industry
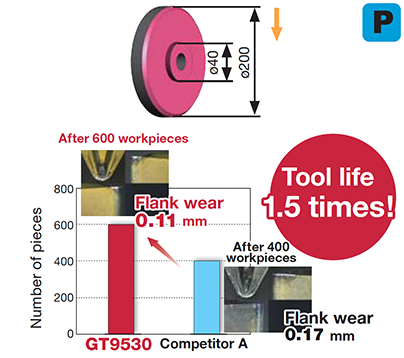
| Part: | Automotive parts |
| Material: | SPCH |
| Insert: | DNMG150408-TSF |
| Grade: | GT9530 |
| Cutting conditions: | Vc = 225 (m/min) f = 0.25 (mm/rev) ap = 0.3 (mm) Application: Face turning (Continuous cutting) Coolant: Wet |
Example #3
Automotive Industry
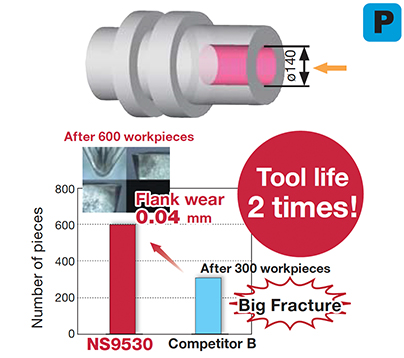
| Part: | Automotive parts |
| Material: | SCM415 |
| Insert: | TPMT110304-PS |
| Grade: | NS9530 |
| Cutting conditions: | Vc = 125 (m/min) f = 0.15 (mm/rev) ap = 1.0 (mm) Application: Internal turning (Continuous cutting) Coolant: Wet |
Standard cutting conditions
NEGATIVE TYPE INSERTS
Basic chipbreaker
| Application | Chipbreaker | Grades | Cutting speedVc (m/min) | Depth of cut ap (mm) |
Feed f(mm/rev) |
||
|---|---|---|---|---|---|---|---|
| Low carbon steels Alloy steels 180HB |
Medium carbon steels Alloy steels 240HB |
High carbon steels Alloy steels 300HB |
|||||
| Precision finishing | TF | NS9530 | 150 — 250 | 80 — 220 | 80 — 180 | 0.1 — 0.5 | 0.03 — 0.15 |
| Finishing | TSF | NS9530 | 150 — 250 | 80 — 220 | 80 — 180 | 0.2 — 1.5 | 0.08 — 0.4 |
| AT9530 | 150 — 300 | 80 — 250 | 80 — 200 | ||||
| GT9530 | 150 — 300 | 80 — 250 | 80 — 200 | ||||
| Finishing to medium cutting |
TS | NS9530 | 150 — 250 | 80 — 220 | 80 — 180 | 0.5 — 2.5 | 0.1 — 0.3 |
| AT9530 | 150 — 300 | 80 — 250 | 80 — 200 | ||||
| GT9530 | 150 — 300 | 80 — 250 | 80 — 200 | ||||
Complementary chipbreakers
| Application | Chipbreaker | Grades | Cutting speedVc (m/min) | Depth of cut ap (mm) |
Feed f(mm/rev) |
||
|---|---|---|---|---|---|---|---|
| Low carbon steels Alloy steels 180HB |
Medium carbon steels Alloy steels 240HB |
High carbon steels Alloy steels 300HB |
|||||
| Precision finishing | 01 | NS9530 | 150 — 250 | 80 — 220 | 80 — 180 | 0.1 — 0.4 | 0.03 — 0.15 |
| A — D | NS9530 | 150 — 250 | 80 — 220 | 80 — 180 | 0.1 — 4.0 | 0.1 — 0.4 | |
| GT9530 | 150 — 300 | 80 — 250 | 80 — 200 | ||||
| W | NS9530 | 150 — 250 | 80 — 220 | 80 — 180 | 0.2 — 1.5 | 0.03 — 0.2 | |
| Finishing | ZF | NS9530 | 150 — 250 | 80 — 220 | 80 — 180 | 0.2 — 1.5 | 0.07 — 0.2 |
| AT9530 | 150 — 300 | 80 — 250 | 80 — 200 | ||||
| GT9530 | 150 — 300 | 80 — 250 | 80 — 200 | ||||
| 11 | NS9530 | 150 — 250 | 80 — 220 | 80 — 180 | 0.2 — 1.5 | 0.07 — 0.2 | |
| GT9530 | 150 — 300 | 80 — 250 | 80 — 200 | ||||
| NS | NS9530 | 150 — 250 | 80 — 220 | 80 — 180 | 0.2 — 1.5 | 0.07 — 0.25 | |
| AFW | NS9530 | 150 — 250 | 80 — 220 | 80 — 180 | 0.5 — 1.5 | 0.2 — 0.4 | |
| GT9530 | 150 — 300 | 80 — 250 | 80 — 200 | ||||
| High feed, small depth of cut |
AS | NS9530 | 150 — 250 | 80 — 220 | 80 — 180 | 0.5 — 2.0 | 0.2 — 0.6 |
| ASW | NS9530 | 150 — 250 | 80 — 220 | 80 — 180 | 0.5 — 2.0 | 0.3 — 0.6 | |
| Boring (Double sided chipbreaker) |
CB | NS9530 | 150 — 250 | 80 — 220 | 80 — 180 | 0.2 — 2.5 | 0.1 — 0.25 |
| GT9530 | 150 — 300 | 80 — 250 | 80 — 200 | ||||
| Finishing to medium cutting |
TM | NS9530 | 150 — 250 | 80 — 220 | 80 — 180 | 0.5 — 5.0 | 0.2 — 0.5 |
| TQ | NS9530 | 150 — 250 | 80 — 220 | 80 — 180 | 0.5 — 2.0 | 0.15 — 0.3 | |
| AT9530 | 150 — 300 | 80 — 250 | 80 — 200 | ||||
| GT9530 | 150 — 300 | 80 — 250 | 80 — 200 | ||||
| ZM | NS9530 | 150 — 250 | 80 — 220 | 80 — 180 | 0.7 — 2.0 | 0.15 — 0.4 | |
| GT9530 | 150 — 300 | 80 — 250 | 80 — 200 | ||||
| NM | NS9530 | 150 — 250 | 80 — 220 | 80 — 180 | 0.5 — 2.0 | 0.15 — 0.4 | |
| GT9530 | 150 — 300 | 80 — 250 | 80 — 200 | ||||
| Medium cutting | All-round | NS9530 | 150 — 250 | 80 — 220 | 80 — 180 | 1.0 — 3.0 | 0.2 — 0.4 |
| GT9530 | 150 — 300 | 80 — 250 | 80 — 200 | ||||
| Parallel | NS9530 | 150 — 250 | 80 — 220 | 80 — 180 | 1.0 — 4.0 | 0.2 — 0.4 | |
| GT9530 | 150 — 300 | 80 — 250 | 80 — 200 | ||||
| S | NS9530 | 150 — 250 | 80 — 220 | 80 — 180 | 1.0 — 4.0 | 0.2 — 0.4 | |
| P | NS9530 | 150 — 250 | 80 — 220 | 80 — 180 | 0.5 — 4.0 | 0.2 — 0.5 | |
POSITIVE TYPE INSERTS
Basic chipbreakers
| Application | Chipbreaker | Grades | Cutting speed Vc (m/min) |
Depth of cut ap (mm) |
Feed f(mm/rev) |
||
|---|---|---|---|---|---|---|---|
| Low carbon steels Alloy steels 180HB |
Medium carbon steels Alloy steels 240HB |
High carbon steels Alloy steels 300HB |
|||||
| Finishing | PSF | NS9530 | 150 — 250 | 80 — 220 | 80 — 180 | 0.1 — 0.5 | 0.05 — 0.3 |
| GT9530 | 150 — 300 | 80 — 250 | 80 — 200 | ||||
| Finishing to light cutting |
PSS | NS9530 | 150 — 250 | 80 — 220 | 80 — 180 | 0.5 — 2.0 | 0.1 — 0.3 |
| GT9530 | 150 — 300 | 80 — 250 | 80 — 200 | ||||
| Finishing to medium cutting |
PS | NS9530 | 150 — 250 | 80 — 220 | 80 — 180 | 0.5 — 2.5 | 0.1 — 0.3 |
| AT9530 | 150 — 300 | 80 — 250 | 80 — 200 | ||||
| GT9530 | 150 — 300 | 80 — 250 | 80 — 200 | ||||
| Medium cutting | PM | NS9530 | 150 — 250 | 80 — 220 | 80 — 180 | 1.0 — 3.0 | 0.15 — 0.3 |
| GT9530 | 150 — 300 | 80 — 250 | 80 — 200 | ||||
Complementary chipbreakers
| Application | Chipbreaker | Grades | Cutting speed Vc (m/min) |
Depth of cut ap (mm) |
Feed f(mm/rev) |
||
|---|---|---|---|---|---|---|---|
| Low carbon steels Alloy steels 180HB |
Medium carbon steels Alloy steels 240HB |
High carbon steels Alloy steels 300HB |
|||||
| Precision finishing | JP | NS9530 | 150 — 250 | 80 — 220 | 80 — 180 | 0.05 — 2.5 | 0.02 — 0.1 |
| AT9530 | 150 — 300 | 80 — 250 | 80 — 200 | ||||
| 01 | NS9530 | 150 — 250 | 80 — 220 | 80 — 180 | 0.05 — 0.5 | 0.03 — 0.15 | |
| GT9530 | 150 — 300 | 80 — 250 | 80 — 200 | ||||
| Finishing | JS | NS9530 | 150 — 250 | 80 — 220 | 80 — 180 | 0.5 — 3 | 0.02 — 0.2 |
| AT9530 | 150 — 300 | 80 — 250 | 80 — 200 | ||||
| PF | NS9530 | 150 — 250 | 80 — 220 | 80 — 180 | 0.1 — 0.5 | 0.05 — 0.25 | |
| GT9530 | 150 — 300 | 80 — 250 | 80 — 200 | ||||
| W08 | NS9530 | 150 — 250 | 80 — 220 | 80 — 180 | 0.1 — 1.0 | 0.03 — 0.15 | |
| GT9530 | 150 — 300 | 80 — 250 | 80 — 200 | ||||
| W10 | NS9530 | 150 — 250 | 80 — 220 | 80 — 180 | 0.1 — 2.0 | 0.03 — 0.2 | |
| GT9530 | 150 — 300 | 80 — 250 | 80 — 200 | ||||
| W11 | NS9530 | 150 — 250 | 80 — 220 | 80 — 180 | 0.1 — 2.0 | 0.03 — 0.2 | |
| W13 | NS9530 | 150 — 250 | 80 — 220 | 80 — 180 | 0.1 — 2.0 | 0.03 — 0.2 | |
| GT9530 | 150 — 300 | 80 — 250 | 80 — 200 | ||||
| W15 | NS9530 | 150 — 250 | 80 — 220 | 80 — 180 | 0.1 — 2.0 | 0.03 — 0.2 | |
| GT9530 | 150 — 300 | 80 — 250 | 80 — 200 | ||||
| W20 | NS9530 | 150 — 250 | 80 — 220 | 80 — 180 | 0.1 — 2.0 | 0.03 — 0.2 | |
| GT9530 | 150 — 300 | 80 — 250 | 80 — 200 | ||||
| with hand | NS9530 | 150 — 250 | 80 — 220 | 80 — 180 | 1.0 — 2.0 | 0.03 — 0.2 | |
| Finishing to medium cutting |
ZF | GT9530 | 150 — 300 | 80 — 250 | 80 — 200 | 0.3 — 1.5 | 0.05 — 0.25 |
| ZM | GT9530 | 150 — 300 | 80 — 250 | 80 — 200 | 0.5 — 2.0 | 0.05 — 0.3 | |
| 23 | NS9530 | 150 — 250 | 80 — 220 | 80 — 180 | 0.5 — 2.0 | 0.1 — 0.3 | |
| SS | NS9530 | 150 — 250 | 80 — 220 | 80 — 180 | 0.5 — 2.0 | 0.1 — 0.3 | |
| All-round | NS9530 | 150 — 250 | 80 — 220 | 80 — 180 | 1.0 — 2.0 | 0.05 — 0.2 | |
| For external turning on small lathes | J10 | NS9530 | 150 — 250 | 80 — 220 | 80 — 180 | 0.1 — 5.0 | 0.01 — 0.1 |
| Medium cutting | 24 | NS9530 | 150 — 250 | 80 — 220 | 80 — 180 | 0.5 — 3.0 | 0.08 — 0.3 |
| Heavy cutting | 61 | NS9530 | 150 — 250 | 80 — 220 | 80 — 180 | 0.2 — 2.0 | 0.3 — 1.0 |
| Finishing to medium cutting | — | NS9530 | 150 — 250 | 80 — 220 | 80 — 180 | 0.1 — 2.0 | 0.05 — 0.3 |
Industries |
|
ПРИМЕНЕНИЕ Учить больше |
e-Catalog |
|
Электронный
каталог Учить больше |
Resources
 Tungaloy APP
 TUNG NaviTool recommendations for your specific needs
 Machine Power Calculator
 Turning Insert Selection Guide
 Tungaloy Success ReportExplore Tungaloy’s TSR for custom machining insights with easy search
 Technical GuidesAccess Tungaloy’s technical guides for valuable insights, references, and resources.
 MatrixTool management system
 Special tool drawing generatorQuickly generate simple drawings for special products.