



PVD grades for heat-resistant alloys
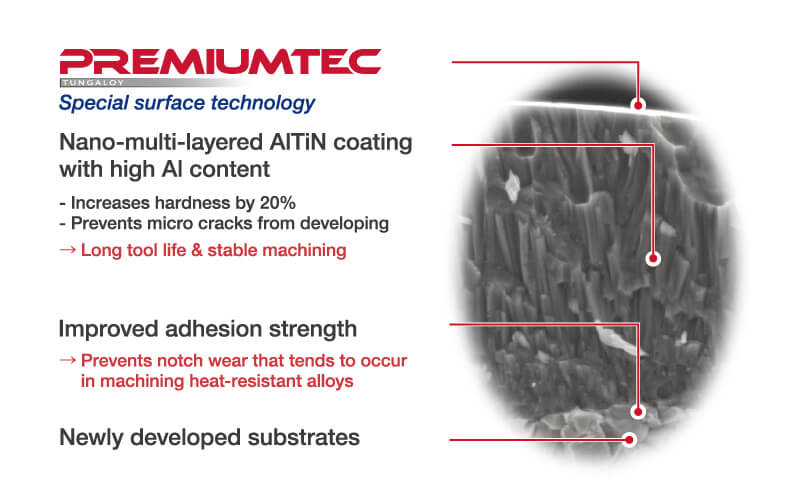
Incredible reliability in turning of heat-resistant alloy due to Nano-multi-layered AlTiN coating with high Al content
Applications & Features
Applications
Features
1. AH8000 series
2. Application area
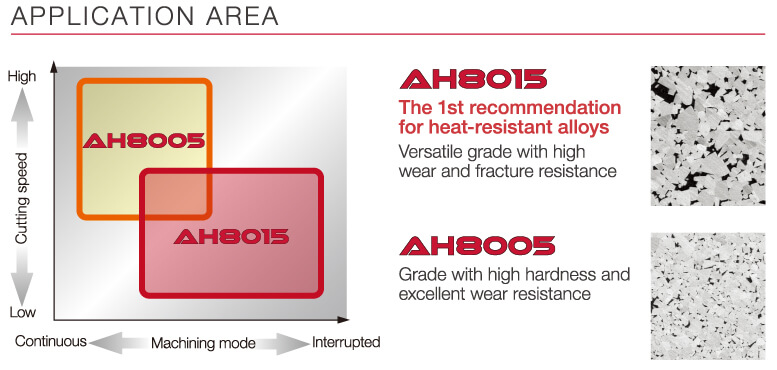
Main Grades
AH8005
- M01 — M10 / S01 — S10
- Good resistance to wear and adhesion
- Excellent performance in machining heat-resistant alloy at high speed
AH8015


- M01 — M20 / S10 — S20
- Good balance between wear and fracture resistance
- First choice for machining heat-resistant alloy under general cutting conditions
Practical examples
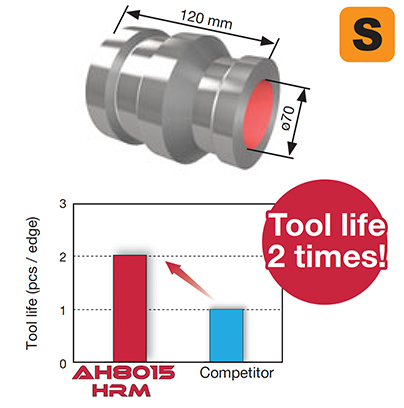
Example #1
Aerospace Industry
| Part: | Aircraft parts |
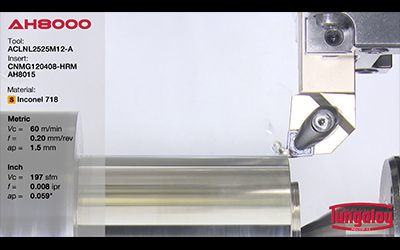
| Material: | Inconel 718 |
| Insert: | CNMG120408-HRM |
| Grade: | AH8015 |
| Cutting conditions: | Vc = 40 (m/min) f = 0.22 (mm/rev) ap = 2.0 (mm) Coolant: Wet |
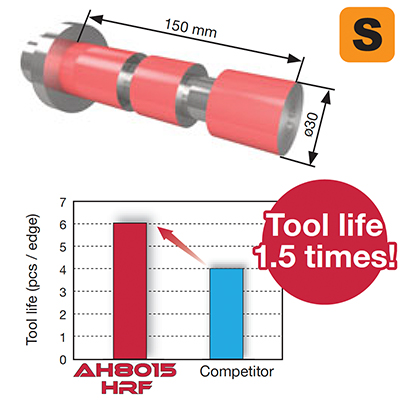
Example #2
Aerospace Industry
| Part: | Aircraft parts |
| Material: | Inconel 909 |
| Insert: | CNMG120412-HRF |
| Grade: | AH8015 |
| Cutting conditions: | Vc = 55 (m/min) f = 0.30 (mm/rev) ap = 0.5 (mm) Coolant: Wet |
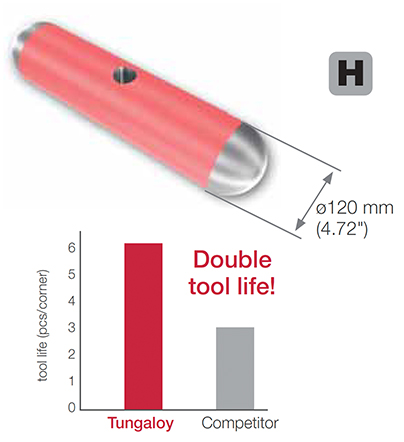
Example #3
General Engineering
| Part: | Toggle pin |
| Material: | Tool steel (49 HRC) |
| Insert: | CNMG190616-HRM |
| Grade: | AH8005 |
| Cutting conditions: | Vc = 66 (m/min) f = 0.6 (mm/rev) ap = 1.25 (mm) Application: External turning Coolant: Dry Machine: NC lathe |
Standard cutting conditions
For negative inserts chipbreaker
| ISO | Chipbreaker | Corner radius RE |
Depth of cut ap (mm) |
Feed f (mm/rev) |
Cutting speed: Vc (m/min) | |
|---|---|---|---|---|---|---|
| AH8005 | AH8015 | |||||
 |
HRF | 0.4 | 0.2 — 1.5 | 0.05 — 0.23 | 40 — 100 | 20 — 80 |
| 0.8 | 0.2 — 1.5 | 0.05 — 0.25 | 40 — 100 | 20 — 80 | ||
| 1.2 | 0.2 — 1.5 | 0.07 — 0.27 | 40 — 100 | 20 — 80 | ||
| HRM | 0.4 | 0.5 — 4 | 0.05 — 0.3 | 40 — 100 | 20 — 80 | |
| 0.8 | 0.5 — 4 | 0.07 — 0.33 | 40 — 100 | 20 — 80 | ||
| 1.2 | 0.5 — 4 | 0.10 — 0.35 | 40 — 100 | 20 — 80 | ||
| 1.6 | 0.5 — 4 | 0.15 — 0.4 | 40 — 100 | 20 — 80 | ||
| SDM | 0.4 | 1 — 4 | 0.2 — 0.3 | 40 — 100 | 20 — 80 | |
| 0.8 | 1 — 4 | 0.2 — 0.5 | 40 — 100 | 20 — 80 | ||
| 1.2 | 1 — 4 | 0.2 — 0.5 | 40 — 100 | 20 — 80 | ||
| 28 | 0.4 | 0.5 — 3 | 0.08 — 0.2 | 40 — 100 | 20 — 80 | |
| 0.8 | 0.5 — 3 | 0.1 — 0.3 | 40 — 100 | 20 — 80 | ||
| 1.2 | 0.5 — 3 | 0.1 — 0.3 | 40 — 100 | 20 — 80 | ||
For positive inserts chipbreaker
| ISO | Chipbreaker | Size | Corner radius RE |
Depth of cut ap (mm) |
Feed f (mm/rev) |
Cutting speed: Vc (m/min) | |
|---|---|---|---|---|---|---|---|
| AH8005 | AH8015 | ||||||
|
PSF | — | 0.4 | 0.05 — 0.5 | 0.02 — 0.2 | 40 — 100 | 20 — 80 |
| — | 0.8 | 0.05 — 0.5 | 0.02 — 0.3 | 40 — 100 | 20 — 80 | ||
| PSS | — | 0.4 | 0.3 — 2 | 0.02 — 0.2 | 40 — 100 | 20 — 80 | |
| — | 0.8 | 0.3 — 2 | 0.03 — 0.3 | 40 — 100 | 20 — 80 | ||
| — | 1.2 | 0.3 — 2 | 0.05 — 0.3 | 40 — 100 | 20 — 80 | ||
| PS | — | 0.4 | 0.5 — 2.5 | 0.02 — 0.2 | 40 — 100 | 20 — 80 | |
| — | 0.8 | 0.5 — 2.5 | 0.03 — 0.3 | 40 — 100 | 20 — 80 | ||
| — | 1.2 | 0.5 — 2.5 | 0.05 — 0.3 | 40 — 100 | 20 — 80 | ||
| PM | — | 0.4 | 1 — 3 | 0.15 — 0.3 | 40 — 100 | 20 — 80 | |
| — | 0.8 | 1 — 3 | 0.15 — 0.3 | 40 — 100 | 20 — 80 | ||
| — | 1.2 | 1 — 3 | 0.15 — 0.3 | 40 — 100 | 20 — 80 | ||
| RS | RCMT06… | — | 0.5 — 2 | 0.2 — 0.6 | 40 — 100 | 20 — 80 | |
| RCMT08… | — | 0.5 — 2 | 0.2 — 0.6 | 40 — 100 | 20 — 80 | ||
| RCMT10… | — | 1 — 2.5 | 0.2 — 0.6 | 40 — 100 | 20 — 80 | ||
| RCMT12… | — | 1 — 2.5 | 0.2 — 0.6 | 40 — 100 | 20 — 80 | ||
| RCMT16… | — | 1.5 — 3 | 0.5 — 1 | 40 — 100 | 20 — 80 | ||
| RCMT20… | — | 1.5 — 3 | 0.5 — 1 | 40 — 100 | 20 — 80 | ||
| RCMT25… | — | 1.5 — 5 | 0.5 — 1 | 40 — 100 | 20 — 80 | ||
| JS | — | < 0.1 | 0.5 — 3 | 0.02 — 0.05 | — | 20 — 80 | |
| — | < 0.2 | 0.5 — 3 | 0.02 — 0.1 | — | 20 — 80 | ||
| — | < 0.4 | 0.5 — 3 | 0.05 — 0.2 | — | 20 — 80 | ||
Metric
Imperial
Industries |
|
ПРИМЕНЕНИЕ Учить больше |
e-Catalog |
|
Электронный
каталог Учить больше |
Resources
 Tungaloy APP
 TUNG NaviTool recommendations for your specific needs
 Machine Power Calculator
 Turning Insert Selection Guide
 Tungaloy Success ReportExplore Tungaloy’s TSR for custom machining insights with easy search
 Technical GuidesAccess Tungaloy’s technical guides for valuable insights, references, and resources.
 MatrixTool management system
 Special tool drawing generatorQuickly generate simple drawings for special products.