


Grinding Cost Reduction Calculator
Grinding Cost Reduction Calculator
This calculator can be used when considering switching from your current grinding process to finishing with CBN/ceramic tools.
By entering values in the following fields, you can calculate the cost savings you would expect from switching to CBN/ceramic tools.
Representative values are pre-filled in each field, but please modify them according to your situation and check the results.
-
Unit
*required fieldsSimulation Results
When using CBN inserts
When using Ceramic inserts
Annual Reduction Amount
0USD per year Reduction Rate
0% Reduction Amount Per Part
0USD per part (Grinding Cost)
0USD per part (Turning Cost)
0USD per part Reduction in Lead Time
0hours per year Reduction in Actual Processing Time
0seconds per part Average Processing Time During Grinding
0seconds per part Average Processing Time During Turning
0seconds per part Number of parts that can be produced with the savings time
0parts per year Recommended Materials and Standard Cutting Conditions
Recommended Feed f (mm/rev):
Application Workpiece Material Grade Cutting Speed Vc (m/min) Depth of Cut ap (mm) Feed f (mm/rev) 
Inconel 718, etc. BX815 80 - 500 0.05 - 0.5 0.05 - 0.3 Titanium Alloy BX480 80 - 200 0.05 - 0.5 0.05 - 0.3 Application Workpiece Material Grade Cutting Speed Vc (m/min) Depth of Cut ap (mm) Feed f (mm/rev) 
Cast Iron BX480 500 - 2000 0.05 - 0.5 0.05 - 0.3 BX5015 100 - 700 0.05 - 0.5 0.05 - 0.3 SBN30 300 - 2000 0.08 - 4 0.05 - 0.5 Ductile Cast Iron BX930 150 - 500 0.05 - 0.5 0.05 - 0.3 Application Grade Workpiece condition Cutting Speed Vc (m/min) Depth of cut ap (mm) Feed f (mm/rev) 
BM05M Continuous 200 - 350 0.05 - 0.2 0.05 - 0.2 BXA10 Continuous 100 - 230 0.05 - 0.5 0.05 - 0.3 Light interrupted 100 - 230 0.05 - 0.3 0.05 - 0.2 BXA20 Interrupted 60 - 180 0.05 - 0.3 0.05 - 0.2 BR35F Heavy interrupted 50 - 150 0.05 - 0.3 0.05 - 0.2 Application Grade Workpiece condition Cutting Speed Vc (m/min) Feed f (mm/rev)
BX360 Continuous 80 - 150 0.03 - 0.08 Light interrupted 50 - 120 0.03 - 0.08 Application Workpiece materials Grade Cutting Speed Vc (m/min) Depth of cut ap (mm) Feed f (mm/rev) Sintered alloy General sintered alloy BX4015 10 - 300 0.05 - 0.5 0.01 - 0.3 Sintered-hardened alloy 10 - 180 0.05 - 0.3 0.01 - 0.2 Application Workpiece materials Grade Cutting Speed Vc (m/min) Depth of cut ap (mm) Feed f (mm/rev) Ni-based super alloys TS200 200 - 350 0.1 - 2 0.1 - 0.4 TS300 150 - 250 0.1 - 2 0.1 - 0.2 Co-based super alloys TS200 200 - 350 0.1 - 2 0.1 - 0.4 TS300 150 - 250 0.1 - 2 0.1 - 0.2 Application Workpiece materials Workpiece Condition Coolant Grade Cutting Speed Vc (m/min) Depth of cut ap (mm) Feed f (mm/rev) Gray cast iron Continuous Dry TZ120 400 - 850 0.5 - 2 0.1 - 0.3 Continuous, Light interrupted Dry LX21 400 - 800 0.5 - 2 0.1 - 0.4 Continuous, Interrupted Dry, Wet FX105 300 - 600 0.5 - 4 0.2 - 0.6 Centrifugal cast iron Continuous Dry TZ120 150 - 400 0.5 - 2 0.1 - 0.3 Application Workpiece materials Workpiece Condition Coolant Grade Cutting Speed Vc (m/min) Depth of cut ap (mm) Feed f (mm/rev) Hardened steel Continuous Wet LX10 50 - 150 0.05 - 2 0.05 - 0.2 Notes and Disclaimers
- The simulation results do not guarantee the actual effects. Please note that the actual effects may vary depending on individual circumstances.
-
Unit
*required fieldsCurrency Unit Workpiece
Application Workpiece Material 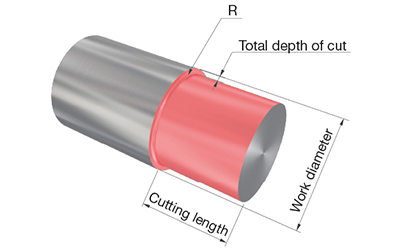
Work Diameter Cutting Length Total Depth of Cut Corner Radius Interrupt Condition Workpiece Material 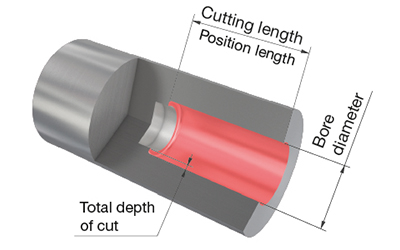
Bore Diameter Cutting Length Total Depth of Cut Corner Radius Interrupt Condition Workpiece Material 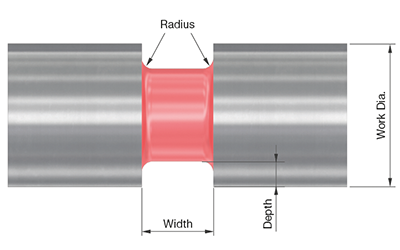
Work Diameter Grooving Depth Grooving Width Corner Radius Interrupt Condition Workpiece Material 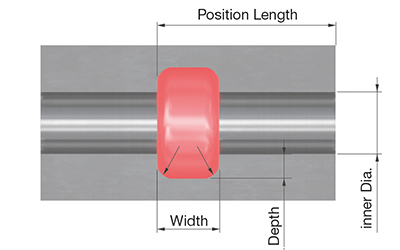
Inner Diameter Groove Depth Groove Width Corner Radius Position Length Interrupt Condition Workpiece Material 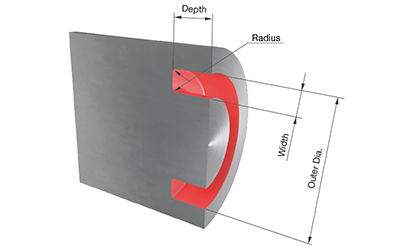
Work Diameter Outer Diameter Groove Width Groove Depth Corner Radius Interrupt Condition Target Surface Roughness Production quantity of parts
Annual production quantity of parts Current Grinding Process Input Items
Machine cost Grinding wheel cost Grinding wheel life Consumable Cost(Coolant, Dressing Tools, etc.) Hourly wage of an operator Average Processing Time Work Exchange Time Input Items When Switching to Turning
Machine Cost Consumable Cost(Coolant etc.) Hourly wage of an operator Work exchange time Other Input Items
Priority LoadingSimulation Results
When using CBN inserts
When using Ceramic inserts
Annual Reduction Amount
0USD per year Reduction Rate
0% Reduction Amount Per Part
0USD per part (Grinding Cost)
0USD per part (Turning Cost)
0USD per part Reduction in Lead Time
0hours per year Reduction in Actual Processing Time
0seconds per part Average Processing Time During Grinding
0seconds per part Average Processing Time During Turning
0seconds per part Number of parts that can be produced with the savings time
0parts per year Recommended Materials and Standard Cutting Conditions
Recommended Feed f (mm/rev):
Application Workpiece materials Grade Cutting Speed Vc (m/min) Depth of cut ap (mm) Feed f (mm/rev) Inconel 718, etc. BX815 80 - 500 0.05 - 0.5 0.05 - 0.3 Titanium Alloy BX480 80 - 200 0.05 - 0.5 0.05 - 0.3 Application Workpiece materials Grade Cutting Speed Vc (m/min) Depth of cut ap (mm) Feed f (mm/rev) Cast Iron BX480 500 - 2000 0.05 - 0.5 0.05 - 0.3 BX5015 100 - 700 0.05 - 0.5 0.05 - 0.3 SBN30 300 - 2000 0.08 - 4 0.05 - 0.5 Ductile Cast Iron BX930 150 - 500 0.05 - 0.5 0.05 - 0.3 Application Grade Workpiece condition Cutting Speed Vc (m/min) Depth of cut ap (mm) Feed f (mm/rev)
BM05M Continuous 200 - 350 0.05 - 0.2 0.05 - 0.2 BXA10 Continuous 100 - 230 0.05 - 0.5 0.05 - 0.3 Light interrupted 100 - 230 0.05 - 0.3 0.05 - 0.2 BXA20 Interrupted 60 - 180 0.05 - 0.3 0.05 - 0.2 BR35F Heavy interrupted 50 - 150 0.05 - 0.3 0.05 - 0.2 Application Grade Workpiece condition Cutting Speed Vc (m/min) Feed f (mm/rev)
BX360 Continuous 80 - 150 0.03 - 0.08 Light interrupted 50 - 120 0.03 - 0.08 Application Workpiece materials Grade Cutting Speed Vc (m/min) Depth of cut ap (mm) Feed f (mm/rev) Sintered alloy General sintered alloy BX4015 10 - 300 0.05 - 0.5 0.01 - 0.3 Sintered-hardened alloy 10 - 180 0.05 - 0.3 0.01 - 0.2 Application Workpiece materials Grade Cutting Speed Vc (m/min) Depth of cut ap (mm) Feed f (mm/rev) Ni-based super alloys TS200 200 - 350 0.1 - 2 0.1 - 0.4 TS300 150 - 250 0.1 - 2 0.1 - 0.2 Co-based super alloys TS200 200 - 350 0.1 - 2 0.1 - 0.4 TS300 150 - 250 0.1 - 2 0.1 - 0.2 Application Workpiece materials Workpiece Condition Coolant Grade Cutting Speed Vc (m/min) Depth of cut ap (mm) Feed f (mm/rev) Gray cast iron Continuous Dry TZ120 400 - 850 0.5 - 2 0.1 - 0.3 Continuous, Light interrupted Dry LX21 400 - 800 0.5 - 2 0.1 - 0.4 Continuous, Interrupted Dry, Wet FX105 300 - 600 0.5 - 4 0.2 - 0.6 Centrifugal cast iron Continuous Dry TZ120 150 - 400 0.5 - 2 0.1 - 0.3 Application Grade Workpiece materials Workpiece Condition Coolant Cutting Speed Vc (m/min) Depth of cut ap (mm) Feed f (mm/rev) Hardened steel Continuous Wet LX10 50 - 150 0.05 - 2 0.05 - 0.2 Other Recommended Tools
Holder: holder description Insert: insert description Notes and Disclaimers
- The simulation results do not guarantee the actual effects. Please note that the actual effects may vary depending on individual circumstances.
Online shop |
|
Online shop Learn more |
e-Catalog |
|
e-Catalog Learn more |
Resources
 Tungaloy APP
 TUNG NaviTool recommendations for your specific needs
 Machine Power Calculator
 Turning Insert Selection Guide
 Tungaloy Success ReportExplore Tungaloy’s TSR for custom machining insights with easy search
 Technical GuidesAccess Tungaloy’s technical guides for valuable insights, references, and resources.
 MatrixTool management system
 Special tool drawing generatorQuickly generate simple drawings for special products.
 High-Feed Milling PortalWhich High-Feed Milling Cutter Is Right for Your Application?