


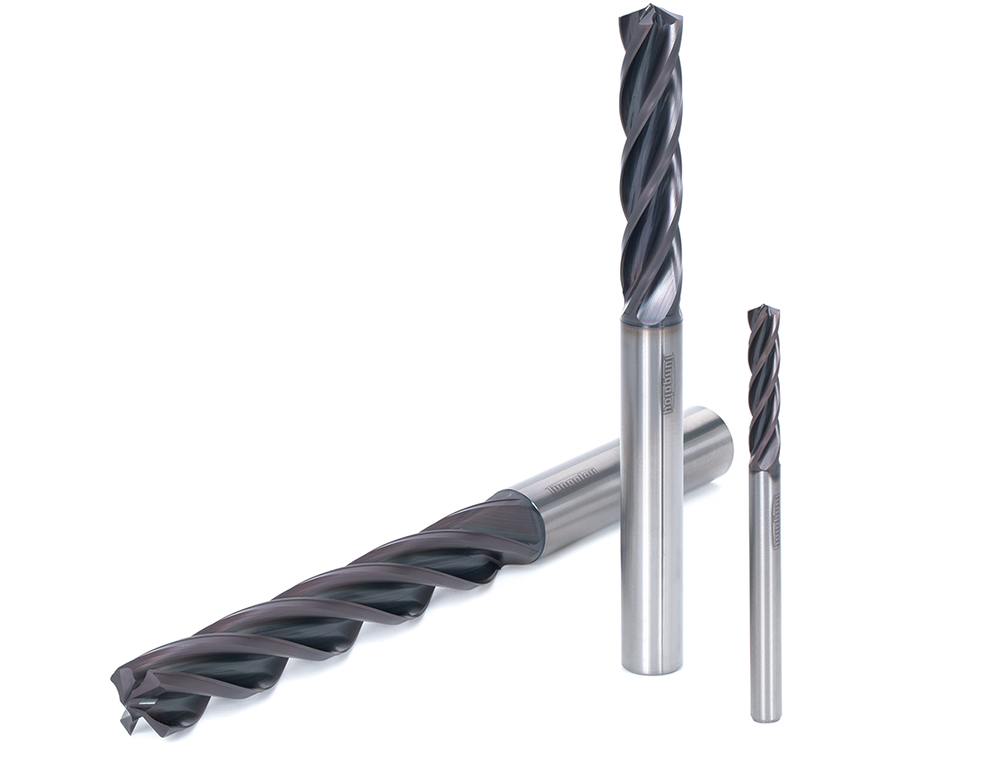
Solid carbide drills with 4 effective cutting edges for superior productivity
Four effective cutting edges for high drilling productivity
Applications & Features
Applications
Features
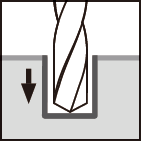
1. Optimized drill edge geometry allows smooth drill entry and stable drilling operations
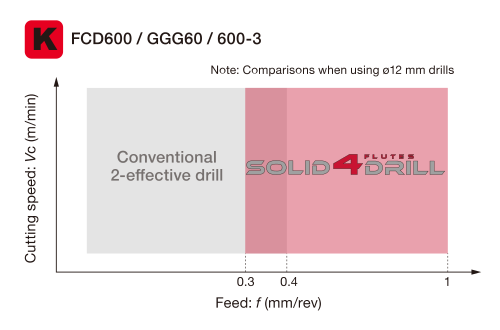
2. Double feed of conventional two-flute drills
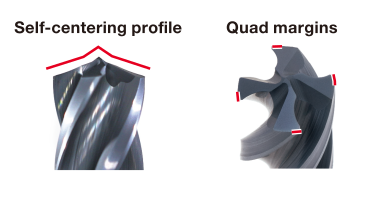
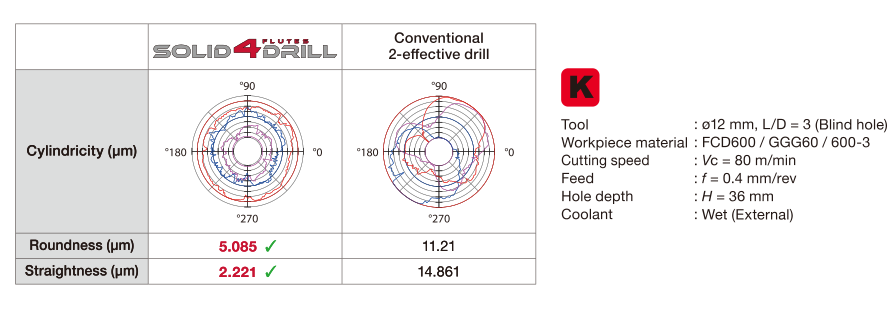
3. Four margins and a self-centering drill geometry enables high hole precision and quality
Drill bodies & Grades
Drill bodies
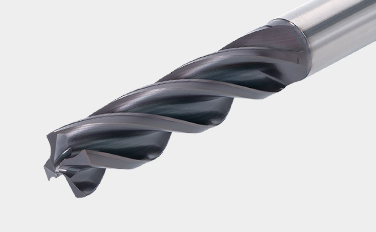
Main Grades
AH9130


- P15 — P35 / M25 — M35 / K10 — K25 / S15 — S30
- High wear resistance
- Designed for drilling various materials
Standard cutting conditions
| ISO | Workpiece material | Brinell hardness
(HB) |
Cutting speed
Vc (m/min) |
Feed: f (mm/rev) | |
|---|---|---|---|---|---|
| ø6 — ø9.9 | ø10 — ø16 | ||||
 |
Grey cast irons FC300, etc. 250, etc. |
— 200 | 60 — 120 | 0.2 — 0.8 | 0.3 -1.0 |
| Ductile cast irons FCD450, etc. 450-10S, etc. |
— 300 | 60 — 120 | 0.2 — 0.8 | 0.3 -1.0 | |
- The cutting parameters shown in the table are a starting guideline.
Values should be varied depending on the power or rigidity of the machine.
Optimum conditions should be selected depending on the actual chip control or damage on edges. - When using the smaller diameter tools in each range, set the feed “f” to the lower values.
- When drilling with a depth deeper than L/D = 3, a pecking cycle or dwell operation should be considered depending on the actual chip control.
e-Catalog
Imperial
Industries |
|
ПРИМЕНЕНИЕ Учить больше |
e-Catalog |
|
Электронный
каталог Учить больше |
Resources
 Tungaloy APP
 TUNG NaviTool recommendations for your specific needs
 Machine Power Calculator
 Turning Insert Selection Guide
 Tungaloy Success ReportExplore Tungaloy’s TSR for custom machining insights with easy search
 Technical GuidesAccess Tungaloy’s technical guides for valuable insights, references, and resources.
 MatrixTool management system
 Special tool drawing generatorQuickly generate simple drawings for special products.