



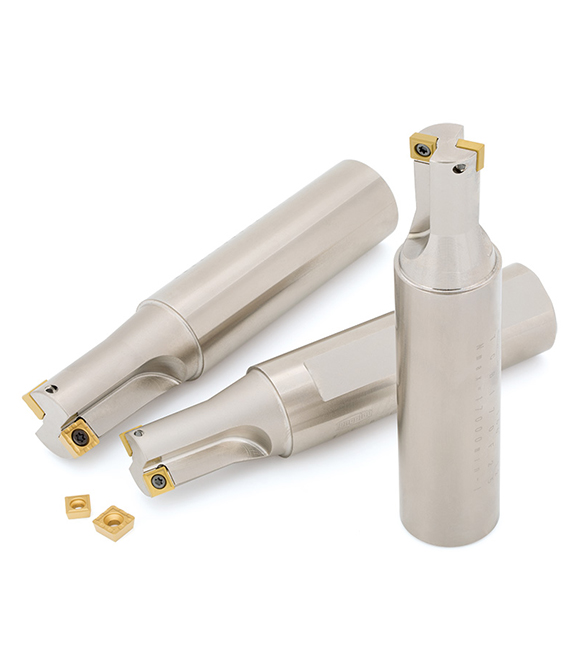
Multifunctional counterboring tool with enriched tool diameter line up
Enriched tool diameter lineup for various hole making operations
Applications & Features
Applications
Features
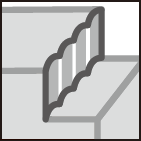
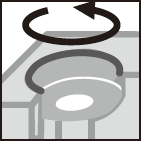
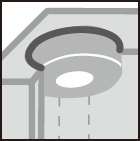
1. Wide variety of tools for various counterboring operations
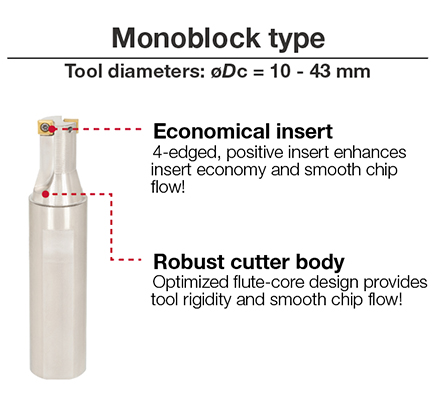
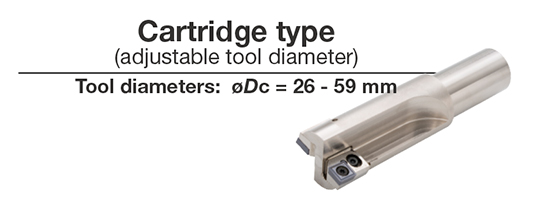
2. 2 types of endmills available
• Mono-block type: ø10 — ø43mm
• Cartridge type: ø26 — ø59mm, Diameter adjustable with shims
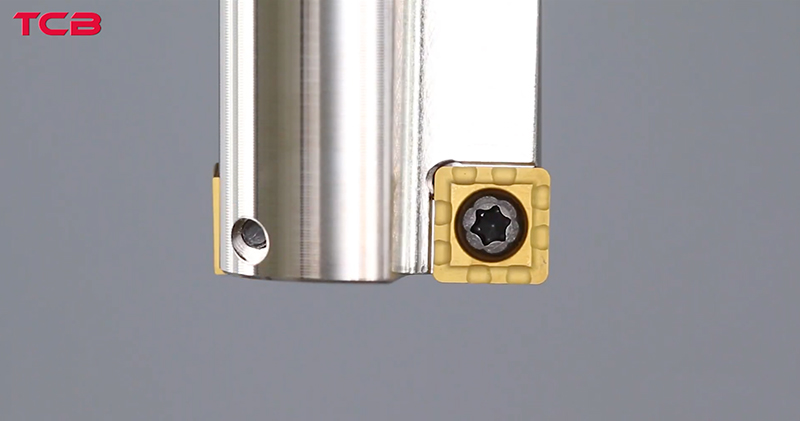
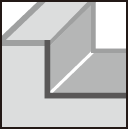
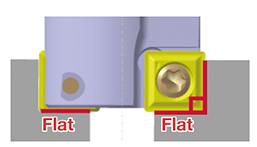
3. Provides a 90° flat surface
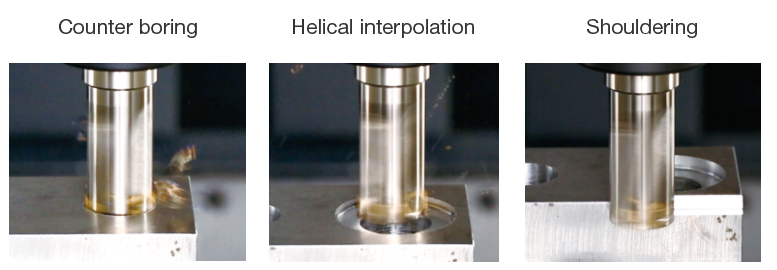
4. Multi-functionality
Inserts & Grades
Inserts
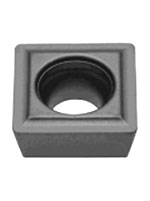
Grades
AH6225


- P20 — P30 / M20 — M30
- First choice for stainless steel
- Excellent versatility for stainless steel machining, demonstrates a good combination of wear and fracture resistance
T313W


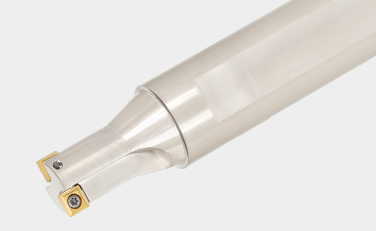
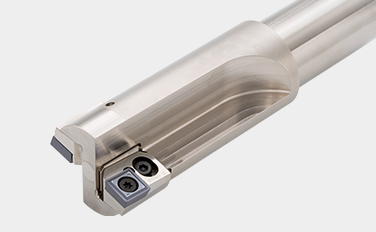
Cutter bodies
Practical examples
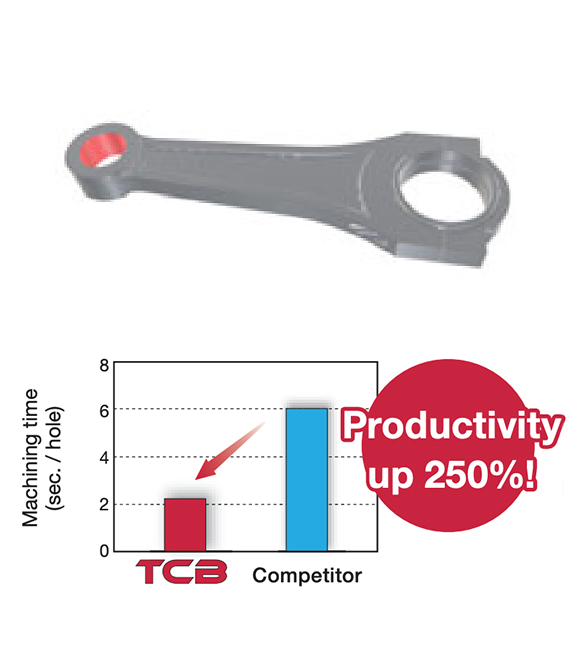
Example #1
Automotive Industry
| Part: | Con-rods |
| Material: | S55C / C55 |
| Drill: | TCB170F25 |
| Insert: | SPMP831DS |
| Grade: | T313W |
| Cutting conditions: | Vc = 160 (m/min) f = 0.2 (mm/rev) Vf = 600 (mm/min) H = 24 (mm) Application: Boring Coolant: Wet Machine: Dedicated machine |
Example #2
General Engineering
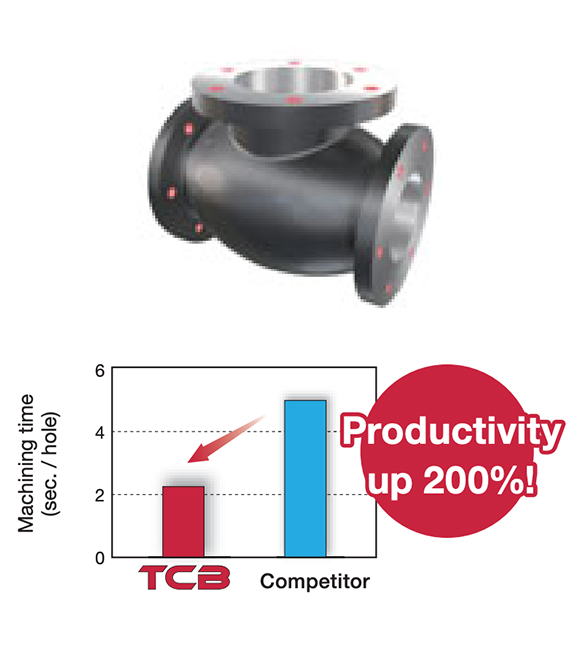
| Part: | Valve |
| Material: | FC250 / GG25 / 250 |
| Drill: | TCB240F25 |
| Insert: | SPMP042ERD |
| Grade: | T313W |
| Cutting conditions: | Vc= 180 (m/min) f= 0.3 (mm/rev) Vf= 720 (mm/min) H= 30 (mm) Application: Boring Coolant: Wet Machine: Horizontal M/C, BT50 |
Example #3
General Engineering
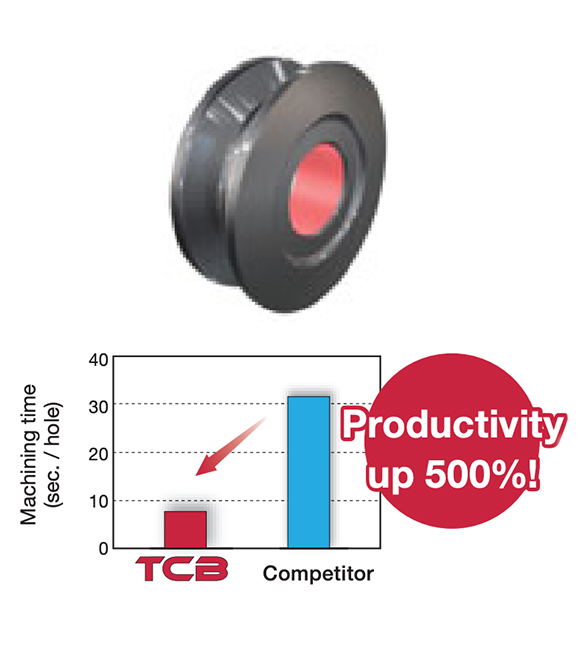
| Part: | Bearing |
| Material: | S45C / C45 |
| Drill: | TCB-320 |
| Insert: | SPMM322ERD |
| Grade: | T313W |
| Cutting conditions: | Vc= 150 (m/min) f= 0.25 (mm/rev) Vf= 375 (mm/min) H= 40 (mm) Application: Boring Coolant: Wet Machine: NC lathe |
Standard cutting conditions
Counter boring
| ISO | Workpiece material | Hardness | Cutting speed Vc (m/min) |
Feed : f (mm/rev) | |
|---|---|---|---|---|---|
| ø10 — 12 (z = 1) | ø13 — 59 (z = 2) | ||||
|
Carbon steel | — 300 HB | 80 — 200 | 0.03 — 0.08 | 0.1 — 0.3 |
|
Stainless steel | — 200 HB | 80 — 150 | 0.03 — 0.05 | 0.06 — 0.15 |
 |
Grey cast iron | 150 — 250 HB | 80 — 200 | 0.05 — 0.1 | 0.1 — 0.4 |
 |
Non-ferrous | — | 100 — 300 | 0.05 — 0.2 | 0.1 — 0.4 |
 |
Superalloys | — 40 HRC | 50 — 80 | 0.03 — 0.05 | 0.06 — 0.15 |
 |
Hard materials | — 50 HRC | 50 — 80 | 0.03 — 0.05 | 0.06 — 0.15 |
Milling
| ISO | Workpiece material | Hardness | Cutting speed Vc (m/min) |
Feed per tooth fz (mm/t) |
|---|---|---|---|---|
|
Carbon steel | — 300 HB | 80 — 200 | 0.05 — 0.15 |
|
Stainless steel | — 200 HB | 80 — 150 | 0.05 — 0.1 |
|
Grey cast iron | 150 — 250 HB | 80 — 200 | 0.05 — 0.2 |
|
Non-ferrous | — | 100 — 300 | 0.1 — 0.2 |
|
Superalloys | — 40 HRC | 50 — 80 | 0.05 — 0.08 |
|
Hard materials | — 50 HRC | 50 — 80 | 0.05 — 0.08 |
Internal boring (With one cutting edge)
| ISO | Workpiece material | Hardness | Cutting speed Vc (m/min) |
Depth of cut ap (mm) |
Feed fz (mm/t) |
|---|---|---|---|---|---|
|
Carbon steel | — 300 HB | 80 — 200 | 0.5 — | 0.05 — 0.15 |
|
Stainless steel | — 200 HB | 80 — 150 | 0.5 — | 0.05 — 0.1 |
|
Grey cast iron | 150 — 250 HB | 80 — 200 | 0.5 — | 0.05 — 0.2 |
|
Non-ferrous | — | 100 — 300 | 0.5 — | 0.1 — 0.2 |
|
Superalloys | — 40 HRC | 50 — 80 | 0.5 — | 0.05 — 0.08 |
|
Hard materials | — 50 HRC | 50 — 80 | 0.5 — | 0.05 — 0.08 |
e-Catalog
Metric
Imperial
Industries |
|
ПРИМЕНЕНИЕ Учить больше |
e-Catalog |
|
Электронный
каталог Учить больше |
Resources
 Tungaloy APP
 TUNG NaviTool recommendations for your specific needs
 Machine Power Calculator
 Turning Insert Selection Guide
 Tungaloy Success ReportExplore Tungaloy’s TSR for custom machining insights with easy search
 Technical GuidesAccess Tungaloy’s technical guides for valuable insights, references, and resources.
 MatrixTool management system
 Special tool drawing generatorQuickly generate simple drawings for special products.