



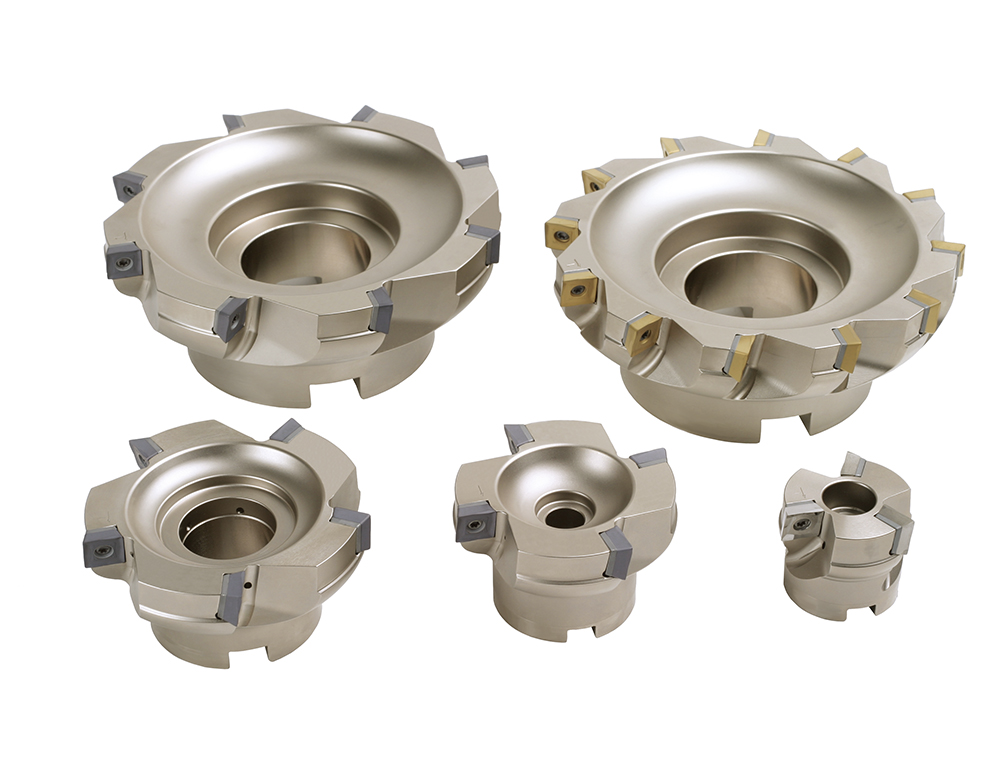
The best solution for steel and cast iron milling
Exact simulation analysis provides light weight cutter with low cutting
Applications & Features
Applications
Features
1. CBN grade inserts for high-speed cast iron machining
High CBN content grade composed of extremely dense medium CBN grains

Inserts & Grades
Inserts
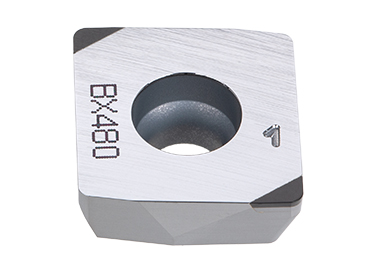
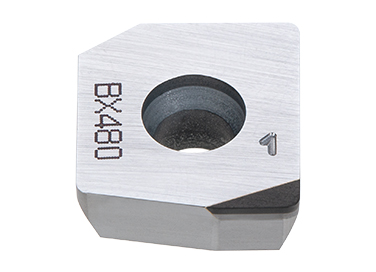
F2-SWGW
- Maximum depth of cut: 0.5 mm
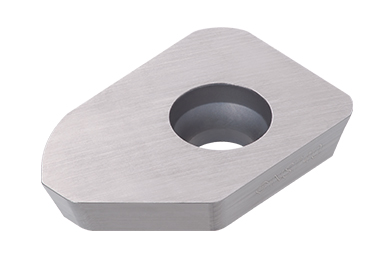
WSGW
- Wiper edge
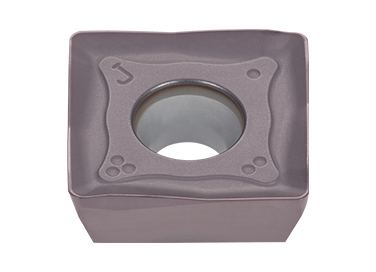
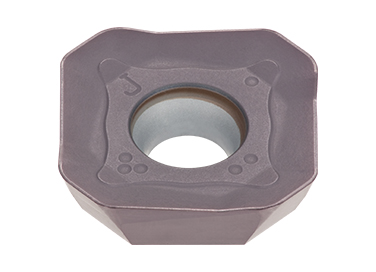
SW*T1304
- Maximum depth of cut: 10 mm
Grades
BX480

- Hardest CBN
- Ideal for ferrous sintered metal
- Suitable for high-speed face milling of cast iron
AH130

- High chipping and fracture resistance
- Designed for machining austenitic stainless steel under general cutting conditions
AH3135

- High fracture resistance
- Suitable for machining steel and stainless steel under general cutting conditions
Cutter bodies
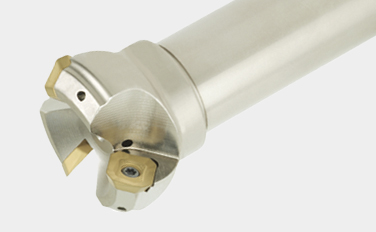
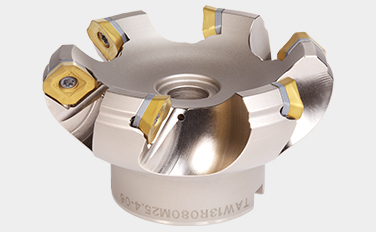
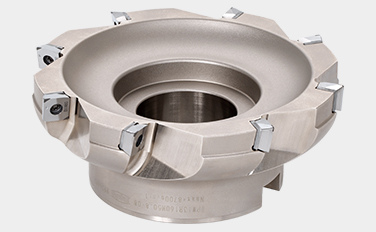
Shank Type
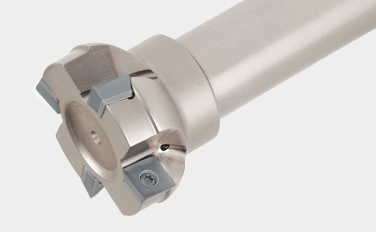
EPW13 (ø32 – ø80mm)
Square shoulder endmill, shank type, with screw clamp system
Practical examples
Example #1
| Part: | Cylinder block |
| Material: | FC250 / 250 |
| Cutter: | TPW13R125M38.1-08 (DCX = 125 mm, CICT = 8) |
| Insert: | 2-SWGW130508PDLSR x6, WSGW130508PDLSR x2 |
| Grade: | BX480 |
| Cutting conditions: | Vc = 800 (m/min) fz = 0.11 (mm/t) Vf = 1,760 (mm/min) ap = 0.2 (mm) ae = ~ 80 (mm) Application: Face milling Coolant: Dry Machine: Horizontal M/C, KM100 |

Example #2
| Part: | Cylinder block |
| Material: | FC250 / 250 |
| Cutter: | TPW13 cutter (customized, DCX = 250 mm, CICT = 12) |
| Insert: | 2-SWGW130508PDLSR x10, WSGW130508PDLSR x2 |
| Grade: | BX480 |
| Cutting conditions: | Vc = 1,178 ~ 1,257 (m/min) fz = 0.05 ~ 0.11 (mm/t) Vf = 900 ~ 1,980 (mm/min) ap = 0.2 (mm) ae = ~ 200 (mm) Application: Face milling Coolant: Dry Machine: Horizontal M/C, KM100 |

Example #3
| Part: | Hydraulic part |
| Material: | Chromium molybdenum steel (SCM415) |
| Cutter: | TPW13R080M25.4-04 (ø80, z=4) |
| Insert: | SWMT1304PDPR-MS |
| Grade: | AH140 |
| Cutting conditions: | Vc = 120 (m/min) fz = 0.18 (mm/t) Vf = 350 (mm/min) ap = 1.2 (mm) ae = ~ 50 (mm) Application: Face milling Coolant: Dry Machine: — |

Standard cutting conditions
TAW13, EAW13
| ISO | Workpiece materials |
Hardness | Priority | Grade | Cutting speed Vc(m/min) |
Roughing (Depth of cut ≥ 1.0 mm) | |||||
|---|---|---|---|---|---|---|---|---|---|---|---|
| Feed per tooth:fz (mm/t) | |||||||||||
| MJ | ML | HJ | MS | Flat top | AJ | ||||||
 |
Mild steel Low carbon steel |
< 180 HB | First choice | AH3225 (AH3135) |
100 — 270 | 0.05 — 0.3 | 0.05 — 0.25 | 0.2 — 0.6 | — | 0.05 — 0.3 | — |
| < 180 HB | Wear resistance | T3225 | 150 — 300 | 0.05 — 0.3 | — | 0.2 — 0.6 | — | 0.05 — 0.3 | — | ||
| < 180 HB | Surface quality | NS740 | 100 — 300 | 0.05 — 0.23 | — | — | — | 0.05 — 0.23 | — | ||
| Carbon steel Alloy steel |
< 300 HB | First choice | AH3225 (AH3135) |
100 — 230 | 0.05 — 0.25 | 0.05 — 0.2 | 0.2 — 0.5 | — | 0.05 — 0.25 | — | |
| < 300 HB | Wear resistance | T3225 | 150 — 280 | 0.05 — 0.25 | — | 0.2 — 0.5 | — | 0.05 — 0.25 | — | ||
| < 300 HB | Surface quality | NS740 | 100 — 230 | 0.05 — 0.2 | — | — | — | 0.05 — 0.2 | — | ||
| Die steel | < 30 HRC | First choice | AH3225 (AH3135) |
100 — 180 | 0.05 — 0.2 | 0.05 — 0.2 | 0.2 — 0.4 | — | 0.05 — 0.2 | — | |
| < 30 HRC | Wear resistance | T3225 | 100 — 180 | 0.05 — 0.2 | — | 0.2 — 0.4 | — | 0.05 — 0.2 | — | ||
 |
Stainless steel | < 250 HB | First choice | AH3135 | 80 — 200 | 0.1 — 0.25 | 0.1 — 0.2 | 0.2 — 0.5 | 0.1 — 0.2 | — | — |
| < 250 HB | Wear resistance | T3225 | 150 — 250 | 0.1 — 0.25 | 0.1 — 0.2 | 0.2 — 0.5 | — | 0.1 — 0.25 | — | ||
 |
Grey cast iron | 150 — 250 HB | First choice | AH8015 (AH120) |
150 — 250 | 0.05 — 0.25 | 0.05 — 0.2 | 0.2 — 0.6 | — | 0.05 — 0.25 | — |
| 150 — 250 HB | Wear resistance | T1215 | 180 — 300 | 0.05 — 0.25 | — | 0.2 — 0.6 | — | 0.05 — 0.25 | — | ||
| Ductile cast iron | 150 — 250 HB | First choice | AH8015 (AH120) |
100 — 180 | 0.05 — 0.25 | 0.05 — 0.2 | 0.2 — 0.6 | — | 0.05 — 0.25 | — | |
| 150 — 250 HB | Wear resistance | T1215 | 120 — 200 | 0.05 — 0.25 | — | 0.2 — 0.6 | — | 0.05 — 0.25 | — | ||
 |
Aluminium alloys Si < 13% |
— | First choice | DS2005 KS05F |
300 — 1000 | — | — | — | — | — | 0.05 — 0.2 |
| — | Wear resistance | DX140 | 200 — 800 | — | — | — | — | — | 0.05 — 0.2 | ||
| Aluminium alloys Si ≥ 13% |
— | First choice | DS2005 KS05F |
80 — 300 | — | — | — | — | — | 0.05 — 0.2 | |
| — | Wear resistance | DX140 | 200 — 800 | — | — | — | — | — | 0.05 — 0.2 | ||
| Copper alloys | — | First choice | DS2005 KS05F |
200 — 500 | — | — | — | — | — | 0.05 — 0.2 | |
| — | Wear resistance | DX140 | 200 — 800 | — | — | — | — | — | 0.05 — 0.2 | ||
 |
Titanium alloys Ti-6Al-4V, etc. |
— 40 HRC | First choice | AH130 | 30 — 60 | 0.1 — 0.25 | — | 0.2 — 0.5 | 0.1 — 0.2 | — | — |
| Heat-resistance alloys Inconel 718, etc. |
— 40 HRC | First choice | AH8015 (AH120) |
20 — 50 | 0.05 — 0.15 | — | 0.1 — 0.3 | — | — | — | |
 |
Hardened steel SKD61, etc. X40CrMoV5-1, etc. |
40 — 50HRC | First choice | AH8015 (AH120) |
45 — 70 | 0.08 — 0.15 | — | 0.1 — 0.3 | — | — | — |
— When using an aggressive depth of cut (for AP or AE), set the Vc and/or fz to the lower side of the value shown in the table.
— Dry cutting (or compressed air) is generally recommended. When excessive chip welding occurs on the cutting edge such as during stainless steel machining, use a water soluble cutting fluid and reduce Vc.
— When wet machining mild steel, carbon steel, or alloy steel, reduce the Vc and/or fz.
— Do not use TAW13 cutters for ramping, plunging, or drilling application as they are not designed for feeding in the Z axis direction.
| ISO | Workpiece materials |
Hardness | Priority | Grade | Cutting speed Vc (m/min) |
Light cutting to finishing (Depth of cut < 1.0 mm) | ||||||
|---|---|---|---|---|---|---|---|---|---|---|---|---|
| Feed per tooth:fz (mm/t) | ||||||||||||
| MJ | ML | HJ | MS | Flat top | AJ | |||||||
|
Mild steel Low carbon steel |
< 180 HB | First choice | AH3225 (AH3135) |
100 — 270 | 0.05 — 0.25 | 0.05 — 0.2 | 0.2 — 0.6 | — | 0.05 — 0.25 | — | |
| < 180 HB | Wear resistance | T3225 | 150 — 300 | 0.05 — 0.25 | — | 0.2 — 0.6 | — | 0.05 — 0.25 | — | |||
| < 180 HB | Surface quality | NS740 | 100 — 300 | 0.05 — 0.2 | — | — | — | 0.05 — 0.23 | — | |||
| Carbon steel Alloy steel |
< 300 HB | First choice | AH3225 (AH3135) |
100 — 230 | 0.05 — 0.2 | 0.05 — 0.25 | 0.2 — 0.5 | — | 0.05 — 0.2 | — | ||
| < 300 HB | Wear resistance | T3225 | 150 — 280 | 0.05 — 0.2 | — | 0.2 — 0.5 | — | 0.05 — 0.2 | — | |||
| < 300 HB | Surface quality | NS740 | 100 — 230 | 0.05 — 0.18 | — | — | — | 0.05 — 0.18 | — | |||
| Die steel | < 30 HRC | First choice | AH3225 (AH3135) |
100 — 180 | 0.05 — 0.18 | 0.05 — 0.12 | 0.2 — 0.4 | — | 0.05 — 0.18 | — | ||
| < 30 HRC | Wear resistance | T3225 | 100 — 180 | 0.05 — 0.18 | — | 0.2 — 0.4 | — | 0.05 — 0.18 | — | |||
|
Stainless steel | < 250 HB | First choice | AH3135 | 80 — 200 | 0.1 — 0.2 | 0.1 — 0.18 | 0.2 — 0.5 | 0.1 — 0.18 | — | — | |
| < 250 HB | Wear resistance | T3225 | 150 — 250 | 0.1 — 0.2 | 0.1 — 0.18 | 0.2 — 0.5 | — | 0.1 — 0.2 | — | |||
|
Grey cast iron | 150 — 250 HB | First choice | AH8015 (AH120) |
150 — 250 | 0.1 — 0.2 | 0.05 — 0.18 | 0.2 — 0.6 | — | 0.1 — 0.2 | — | |
| 150 — 250 HB | Wear resistance | T1215 | 180 — 300 | 0.1 — 0.2 | — | 0.2 — 0.6 | — | 0.1 — 0.2 | — | |||
| Ductile cast iron | 150 — 250 HB | First choice | AH8015 (AH120) |
100 — 180 | 0.1 — 0.2 | 0.05 — 0.18 | 0.2 — 0.6 | — | 0.1 — 0.2 | — | ||
| 150 — 250 HB | Wear resistance | T1215 | 120 — 200 | 0.1 — 0.2 | — | 0.2 — 0.6 | — | 0.1 — 0.2 | — | |||
|
Aluminium alloys Si < 13% |
— | First choice | DS2005 KS05F |
300 — 1000 | — | — | — | — | — | 0.05 — 0.2 | |
| — | Wear resistance | DX140 | 200 — 800 | — | — | — | — | — | 0.05 — 0.2 | |||
| Aluminium alloys Si ≥ 13% |
— | First choice | DS2005 KS05F |
80 — 300 | — | — | — | — | — | 0.05 — 0.2 | ||
| — | Wear resistance | DX140 | 200 — 800 | — | — | — | — | — | 0.05 — 0.2 | |||
| Copper alloys | — | First choice | DS2005 KS05F |
200 — 500 | — | — | — | — | — | 0.05 — 0.2 | ||
| — | Wear resistance | DX140 | 200 — 800 | — | — | — | — | — | 0.05 — 0.2 | |||
|
Titanium alloys Ti-6Al-4V, etc. |
— 40 HRC | First choice | AH130 | 30 — 60 | 0.1 — 0.21 | — | 0.2 — 0.5 | 0.1 — 0.2 | — | — | |
| Heat-resistance alloys Inconel 718, etc. |
— 40 HRC | First choice | AH8015 (AH120) |
20 — 50 | 0.05 — 0.15 | — | 0.1 — 0.3 | — | — | — | ||
|
Hardened steel |
SKD61, etc. X40CrMoV5-1, etc. |
40 — 50HRC | First choice | AH8015 (AH120) |
45 — 70 | 0.08 — 0.15 | — | 0.1 — 0.3 | — | — | — |
| SKD11, etc. X153CrMoV12, etc. |
50 — 60HRC | First choice | AH8015 (AH120) |
40 — 65 | 0.05 — 0.1 | — | 0.05 — 0.14 | — | — | — | ||
— When using an aggressive depth of cut (for AP or AE), set the Vc and/or fz to the lower side of the value shown in the table.
— Dry cutting (or compressed air) is generally recommended. When excessive chip welding occurs on the cutting edge such as during stainless steel machining, use a water soluble cutting fluid and reduce Vc.
— When wet machining mild steel, carbon steel, or alloy steel, reduce the Vc and/or fz.
— Do not use TAW13 cutters for ramping, plunging, or drilling application as they are not designed for feeding in the Z axis direction.
TPW13, EPW13
| ISO | Workpiece materials |
Hardness | Priority | Grade | Cutting speed Vc (m/min) |
Roughing (Depth of cut ≥ 1.0 mm) | ||||
|---|---|---|---|---|---|---|---|---|---|---|
| Feed per tooth:fz (mm/t) | ||||||||||
| MJ | ML | MS | AJ | |||||||
|
Mild steel Low carbon steel |
< 180 HB | First choice | AH3225 (AH3135) |
100 — 270 | 0.05 — 0.25 | 0.05 — 0.2 | — | — | |
| < 180 HB | Wear resistance | T3225 | 150 — 300 | 0.05 — 0.25 | — | — | — | |||
| < 180 HB | Fracture resistance | AH3135 | 80 — 180 | 0.05 — 0.25 | — | 0.05 — 0.2 | — | |||
| < 180 HB | Surface finish | NS740 | 100 — 300 | 0.05 — 0.15 | — | — | — | |||
| Carbon steel Alloy steel |
< 300 HB | First choice | AH3225 (AH3135) |
100 — 230 | 0.05 — 0.2 | 0.05 — 0.15 | — | — | ||
| < 300 HB | Wear resistance | T3225 | 150 — 280 | 0.05 — 0.2 | — | — | — | |||
| < 300 HB | Fracture resistance | AH3135 | 80 — 150 | 0.05 — 0.2 | — | — | — | |||
| < 300 HB | Surface finish | NS740 | 100 — 230 | 0.05 — 0.15 | — | — | — | |||
| Die steel | < 30 HRC | First choice | AH3225 (AH3135) |
100 — 180 | 0.05 — 0.15 | 0.05 — 0.12 | — | — | ||
| < 30 HRC | Wear resistance | T3225 | 100 — 180 | 0.05 — 0.15 | — | — | — | |||
|
Stainless steel | < 50 HB | First choice | AH3135 | 80 — 200 | 0.05 — 0.2 | — | 0.05 — 0.18 | — | |
| < 50 HB | Wear resistance | T3225 | 150 — 250 | 0.05 — 0.2 | — | — | — | |||
|
Grey cast iron | 150 — 250 HB | First choice | AH8015 (AH120) |
100 — 250 | 0.05 — 0.2 | 0.05 — 0.15 | — | — | |
| 150 — 250 HB | Wear resistance | T1215 | 100 — 250 | 0.05 — 0.2 | — | — | — | |||
| 150 — 250 HB | Use when high efficiency milling is required |
BX480 | 800 — 1500 | 0.05 — 0.3 (F2-SWGW1305) |
— | — | — | |||
| Ductile cast iron | 150 — 250 HB | First choice | AH8015 (AH120) |
100 — 250 | 0.05 — 0.2 | 0.05 — 0.15 | — | — | ||
| 150 — 250 HB | Wear resistance | T1215 | 100 — 250 | 0.05 — 0.2 | — | — | — | |||
|
Aluminium alloys Si < 13% |
— | First choice | DS2005 KS05F |
300 — 1000 | — | — | — | 0.05 — 0.2 | |
| Aluminium alloys Si ≥ 13% |
— | First choice | DS2005 KS05F |
80 — 300 | — | — | — | 0.05 — 0.2 | ||
| Copper alloys | — | First choice | DS2005 KS05F |
200 — 500 | — | — | — | 0.05 — 0.2 | ||
|
Titanium alloys Ti-6Al-4V, etc. |
— 40 HRC | First choice | AH130 | 30 — 60 | 0.1 — 0.25 | — | 0.1 — 0.2 | — | |
| Heat-resistance alloys Inconel 718, etc. |
— 40 HRC | First choice | AH8015 (AH120) |
20 — 50 | 0.05 — 0.15 | 0.05 — 0.1 | — | — | ||
|
Hardened steel |
SKD61, etc. X40CrMoV5-1, etc. |
40 — 50HRC | First choice | AH8015 (AH120) |
45 — 70 | 0.08 — 0.15 | — | — | — |
| SKD11, etc. X153CrMoV12, etc. |
50 — 60HRC | First choice | AH8015 (AH120) |
40 — 65 | 0.06 — 0.1 | — | — | — | ||
— When using an aggressive depth of cut (for AP or AE), set the Vc and/or fz to the lower side of the value shown in the table.
— Dry cutting (or compressed air) is generally recommended. When excessive chip welding occurs on the cutting edge such as during stainless steel machining, use a water soluble cutting fluid and reduce Vc.
— When wet machining mild steel, carbon steel, or alloy steel, reduce the Vc and/or fz.
— Do not use TPW13 cutters for ramping, plunging, or drilling application as they are not designed for feeding in the Z axis direction.
| ISO | Workpiece materials |
Hardness | Priority | Grade | Cutting speed Vc (m/min) |
Light cutting to fi nishing (Depth of cut < 1.0 mm) | |||
|---|---|---|---|---|---|---|---|---|---|
| Feed per tooth:fz (mm/t) | |||||||||
| MJ | ML | MS | AJ | ||||||
|
Mild steel Low carbon steel |
< 180 HB | First choice | AH3225 (AH3135) |
100 — 270 | 0.05 — 0.2 | 0.05 — 0.18 | — | — |
| < 180 HB | Wear resistance | T3225 | 150 — 300 | 0.05 — 0.2 | — | — | — | ||
| < 180 HB | Fracture resistance | AH3135 | 80 — 180 | 0.05 — 0.2 | — | 0.05 — 0.18 | — | ||
| < 180 HB | Surface finish | NS740 | 100 — 300 | 0.05 — 0.12 | — | — | — | ||
| Carbon steel Alloy steel |
< 300 HB | First choice | AH3225 (AH3135) |
100 — 230 | 0.05 — 0.18 | 0.05 — 0.12 | — | — | |
| < 300 HB | Wear resistance | T3225 | 150 — 280 | 0.05 — 0.18 | — | — | — | ||
| < 300 HB | Fracture resistance | AH3135 | 80 — 150 | 0.05 — 0.18 | — | — | — | ||
| < 300 HB | Surface finish | NS740 | 100 — 230 | 0.05 — 0.12 | — | — | — | ||
| Die steel | < 30 HRC | First choice | AH3225 (AH3135) |
100 — 180 | 0.05 — 0.12 | 0.05 — 0.1 | — | — | |
| < 30 HRC | Wear resistance | T3225 | 100 — 180 | 0.05 — 0.12 | — | — | — | ||
|
Stainless steel | < 50 HB | First choice | AH3135 | 80 — 200 | 0.05 — 0.18 | — | 0.05 — 0.15 | — |
| < 50 HB | Wear resistance | T3225 | 150 — 250 | 0.05 — 0.18 | — | — | — | ||
|
Grey cast iron | 150 — 250 HB | First choice | AH8015 (AH120) |
100 — 250 | 0.05 — 0.18 | 0.05 — 0.12 | — | — |
| 150 — 250 HB | Wear resistance | T1215 | 100 — 250 | 0.05 — 0.18 | — | — | — | ||
| Ductile cast iron | 150 — 250 HB | First choice | AH8015 (AH120) |
100 — 250 | 0.05 — 0.18 | 0.05 — 0.12 | — | — | |
| 150 — 250 HB | Wear resistance | T1215 | 100 — 250 | 0.05 — 0.18 | — | — | — | ||
|
Aluminium alloys Si < 13% |
— | First choice | DS2005 KS05F |
300 — 1000 | — | — | — | 0.05 — 0.2 |
| Aluminium alloys Si ≥ 13% |
— | First choice | DS2005 KS05F |
80 — 300 | — | — | — | 0.05 — 0.2 | |
| Copper alloys | — | First choice | DS2005 KS05F |
200 — 500 | — | — | — | 0.05 — 0.2 | |
|
Titanium alloys Ti-6Al-4V, etc. |
— 40 HRC | First choice | AH130 | 30 — 60 | 0.1 — 0.25 | — | 0.1 — 0.25 | — |
| Heat-resistance alloys Inconel 718, etc. |
— 40 HRC | First choice | AH8015 (AH120) |
20 — 50 | 0.05 — 0.15 | 0.05 — 0.1 | — | — | |
|
Hardened SKD61, etc. X40CrMoV5-1, etc. |
40 — 50HRC | First choice | AH8015 (AH120) |
45 — 70 | 0.05 — 0.15 | — | — | — |
— When using an aggressive depth of cut (for AP or AE), set the Vc and/or fz to the lower side of the value shown in the table.
— Dry cutting (or compressed air) is generally recommended. When excessive chip welding occurs on the cutting edge such as during stainless steel machining, use a water soluble cutting fluid and reduce Vc.
— When wet machining mild steel, carbon steel, or alloy steel, reduce the Vc and/or fz.
— Do not use TPW13 cutters for ramping, plunging, or drilling application as they are not designed for feeding in the Z axis direction.
Industries |
|
ПРИМЕНЕНИЕ Учить больше |
e-Catalog |
|
Электронный
каталог Учить больше |
Resources
 Tungaloy APP
 TUNG NaviTool recommendations for your specific needs
 Machine Power Calculator
 Turning Insert Selection Guide
 Tungaloy Success ReportExplore Tungaloy’s TSR for custom machining insights with easy search
 Technical GuidesAccess Tungaloy’s technical guides for valuable insights, references, and resources.
 MatrixTool management system
 Special tool drawing generatorQuickly generate simple drawings for special products.